

To comply with local environmental protection policies and meet the needs of capacity upgrading, we carried out an upgrade and retrofit of the kiln-tail bag filter on a 3,000 t/d cement production line. The goal was to achieve ultra-low emissions and improve energy efficiency while reducing carbon output. The kiln-tail exhaust gas treatment system originally used a high-temperature-resistant, low-pressure pulse jet bag filter with an outlet emission concentration of ≤30 mg/Nm³. Before the retrofit, the system had issues such as excessive particulate emissions and excessively high operating resistance, making it unable to meet the requirements of the production process. The main technical parameters are shown in the table below. Through our upgrade, including increasing the filtration area of the dust collector and replacing the pulsing system, we successfully reduced the particulate emission concentration to below 10 mg/Nm³.
| Airflow Processing Capacity(m³/h) | Inlet Dust Concentration(g/Nm³) | Outlet Dust Concentration(mg/Nm³) | Filter Bag Dimension(mm) | Filtration Area(m²) | Filtration Air Speed(m/min) | MWP(Pa) | Pressure Loss(Pa) |
| 510000 | ≤200 | ≤30 | Ø160×6000 | 9260 | 0.92 | 6500 | 1500-1800 |
Retrofit Scheme
Overall Retrofit: The equipment casing was raised by 2 meters, and the filter bags, bag cages, pulsing system, clean air chamber, and all top components were removed. The equipment was then transformed into a low-pressure, long-bag pulse jet bag filter with a high clean air chamber structure. After the retrofit, the filtration area of the bag filter increased to 11,324 m², and the filtration airspeed was reduced to 0.75 m/min.
Retrofit Scheme
Casing Retrofit: To increase the filtration area and reduce the filtration airspeed, the filter bags were extended to 8 meters, and the equipment casing was raised by 2 meters. The clean air chamber was also increased to a height of 3.2 meters. The bag cages were modified to a sectional design, making it easier for workers to replace them during maintenance inside the clean air chamber.
Filter Bag Replacement: To meet ultra-low emission standards, all the original aramid filter bags were replaced with fiberglass membrane-coated filter bags. The polytetrafluoroethylene (PTFE) microporous membrane can block particles with a larger diameter than the pore size of the membrane, providing very high filtration efficiency. This material is ideal for its high-temperature resistance, corrosion resistance, and ease of dust removal.
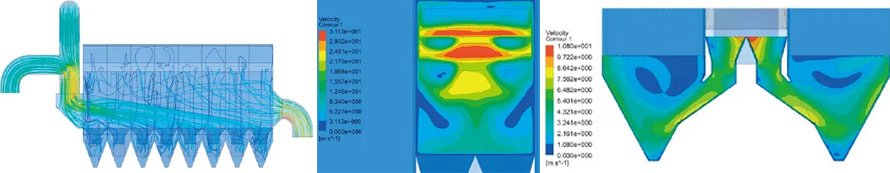
Inlet Guide System Retrofit: The original bag filter used a hopper-based inlet, which resulted in a high operating resistance of up to 2,125 Pa. To reduce the equipment resistance and ensure uniform airflow distribution into the baghouse, we added guide plates to the inlet piping and modified the hopper inlet piping to optimize the airflow distribution inside the equipment. As a result, the resistance of the dust collector was reduced by 380 Pa. We enlarged the inlet cross-section of the wind collection box to lower the inlet airspeed and installed guide arc plates in the inlet piping and wind collection box. The hopper-side inlet piping was modified to increase the inlet cross-sectional area, ensuring that the airflow inside the dust collector was smooth and uniform, with minimal vortex formation. This resulted in a more even airspeed distribution at the inlet section of the dust collector.
Low-pressure Control System: The retrofit adopts the P1000 intelligent control system. This system is based on the distributed control concept and integrates signals from each chamber’s pulse valve, lifting valve, pressure, differential pressure, and other parameters for independent control. It is easy to install and maintain, significantly reducing electrical costs.
Corrosion Protection Measures: The retrofit includes strict requirements for the welding of the filter head plates and the clean air chamber. All weld seams are subjected to kerosene leakage testing. Any defective welds are re-welded and re-tested to ensure that all seams are properly sealed. Additionally, all areas of the dust collector that come into contact with flue gas are coated with anti-corrosion paint.
Retrofit Technical Analysis
Increase In Filtration Area
The methods for increasing the filtration area in this retrofit project mainly include:
1. Increasing the casing height and lengthening the filter bags to expand the filtration area, while keeping the equipment casing foundation unchanged. This approach was adopted for this retrofit.
2. Increasing the number of baghouses where site conditions permit. One method involves adding two small baghouses in series at the rear of the bag filter without adding a new collector. Another method involves adding a small bag filter in parallel next to the original bag filter.
Filter Bag Material Replacement
The filter bag is the core filtration component of a bag dust collector, and the selection of filter bag material is crucial for achieving ultra-low emissions. For this retrofit, we selected fiberglass membrane-coated filter bags that offer high permeability, low resistance, high-temperature resistance (can operate continuously at 260°C), corrosion resistance, and high filtration efficiency. To meet the ultra-low emission requirements, we requested that the manufacturer apply adhesive sealing treatment to the needle holes of the filter bag seams. Additionally, the spring cuff and sewing process for the bag opening were carefully designed, with strict control of assembly tolerances to ensure a proper seal at the bag opening.
Corrosion Protection
1. Based on the characteristics of the flue gas, especially the SO₂ and H₂O content, appropriate anti-corrosion measures must be taken. These include specifying the rust-removal grade, selecting the proper primer, determining the number of coating layers and their thickness, and ensuring proper application. The temperature resistance of the paint must exceed the highest flue gas temperature to prevent coating failure caused by overheating.
Under highly corrosive conditions, bag cages generally should not be galvanized; instead, they should be coated with asphalt paint or high-temperature, moisture-resistant paint. A commonly used method today is applying an organosilicon coating to the surface of the bag cages, which is particularly suitable for dust with corrosive properties.
The internal surfaces of the baghouse that come into contact with flue gas, as well as internal components such as blow pipes, should also be coated with anti-corrosion paint. Alternatively, the materials of components exposed to flue gas can be replaced with corrosion-resistant stainless steel.
2. The sealing performance of the bag filter depends on the integrity of its casing. We must ensure high-quality fabrication and installation, and all joints on the casing must be continuously welded. The access doors should be sealed with corrosion-resistant sealing materials.
3. Reduce the moisture content of the gas and increase its temperature to widen the difference between the gas temperature and the dew point. If the air-leakage rate is high, the gas temperature must be at least 30 °C above the dew point. For dust collection equipment used in kiln and coal mill systems, comprehensive external insulation is required to avoid condensation risks. Production operating temperatures should be kept 20–30 °C above the dew point to prevent bag clogging as well as condensation and corrosion.
Retrofit Results
| Item | Working Parameter | Alarm Value |
| O₂ content at outlet C1 | 2~6% | |
| CO content at outlet C1 | 0~0.4% | 0.5H,1HH |
| Temperature at outlet C1-1 | 280~360 ℃ | 400H |
| Negative pressure at outlet C1-1 | -4700~-5500Pa | |
| Temperature at outlet C1-2 | 280~360 ℃ | 400H |
| Negative pressure at outlet C1-2 | -4700~-5500Pa | |
| Temperature at outlet C2 | 450~600 ℃ | |
| Negative pressure at outlet C2 | -3600~-4200Pa | |
| Temperature at outlet C3 | 580~750 ℃ | |
| Negative pressure at outlet C3 | -2800~-3400Pa | |
| Negative pressure at cone C3 | -1500~-3800Pa | -500L |
| Temperature at outlet C4 | 700~850 ℃ | |
| Negative pressure at outlet C4 | -2000~-2700Pa | |
| Negative pressure at cone C4 | -1500~-2000Pa | -400L |
| Material temperature at C4 | 650~760 ℃ | |
| Temperature at outlet C5 | 800~900 ℃ | 900H |
| Negative pressure at outlet C5 | -1500~-2200Pa | |
| Negative pressure at cone C5 | -800~-1500Pa | -300L |
| Material temperature at C5 | 750~860 ℃ | |
| Precalciner outlet temperature | 820~920 ℃ | |
| Precalciner outlet negative pressure | -800~-1200Pa | |
| Precalciner central temperature | 850~950 ℃ | |
| Tertiary air temperature | 700~900 ℃ | |
| Tertiary air duct negative pressure | -100~-500Pa | |
| Kiln tail temperature | 900~1100 ℃ | |
| Kiln tail negative pressure | -300~-600Pa |
